Industrial-Grade Corrugated Packaging Portfolio
Engineered for high-stacking performance, sea-freight durability, and direct-to-consumer unboxing excellence. Designed specifically to endure Mumbai's coastal humidity and intense supply chain handling.
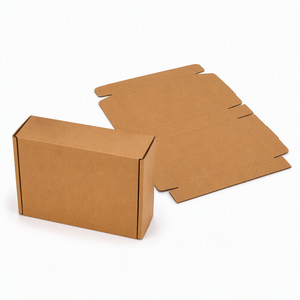
Eco Friendly Biodegradable Kraft Mailer Boxes
Heavy-duty B-flute biodegradable mailers with custom logo printing for ecommerce fulfillment across Western India.
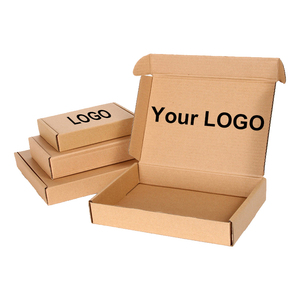
Custom Embossed Kraft Shipping Box Envelope
Long narrow structural profile featuring tactile embossing for premium apparel, cosmetics, and document dispatches.
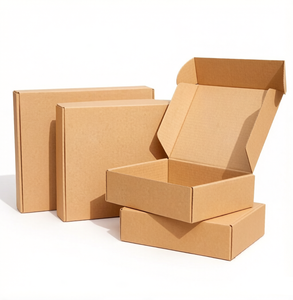
OEM Custom Corrugated E-Commerce Mailer Box
Precision die-cut E-flute corrugated boxes engineered for high-speed automated picking line operations.
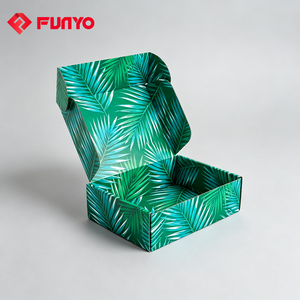
Low MOQ Custom Printed Candle Shipping Boxes
Reinforced double-wall internal structure designed to absorb drop shocks during retail and DTC delivery.
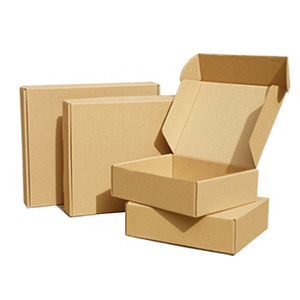
Factory Direct Durable Foldable Kraft Express Box
High-burst-factor corrugated containers optimized for heavy domestic logistics and export consolidation hubs.
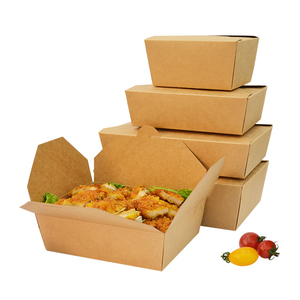
UV Coated Kraft Food-Grade Takeaway Containers
Grease-resistant, oil-proof food delivery packaging compliant with international food contact sanitation codes.
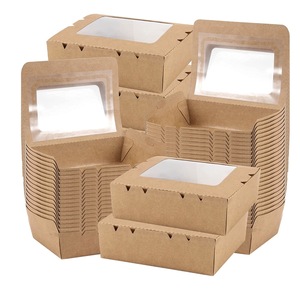
Kraft Brown Food Boxes with PET Clear Windows
High-clarity anti-fog window cartons for bakery, confectionery, and ready-to-eat meal presentation.
Matte UV Magnetic Closure Cardboard Gift Folders
Rigid-corrugated hybrid construction wrapped in premium art paper with hidden magnetic closing clasps.
Corrugated Box Manufacturing Excellence Serving Mumbai’s Enterprise Supply Chains
As a leading custom packaging manufacturer and exporter catering directly to Mumbai’s bustling industrial hubs—ranging from the warehousing mega-complexes in Bhiwandi and Taloja to the high-tech MIDC belts in Thane-Belapur and Tarapur—we deliver structurally superior, eco-conscious corrugated solutions. In an urban industrial ecosystem where ambient humidity levels frequently exceed 85% during the monsoon season, off-the-shelf cardboard packaging fails due to rapid moisture absorption and compression degradation. Our manufacturing methodology addresses these precise regional challenges through advanced paperboard physics, specialized moisture-barrier coatings, and high Edge Crush Test (ECT) ratings.
Information Gain Insight: Standard recycled corrugated boxes lose up to 40% of their stacking strength within 72 hours of exposure to Mumbai's coastal humidity. Our proprietary wet-strength resin formulations and high-density virgin kraft liners preserve up to 94% of structural integrity under extreme damp storage conditions.
High ECT & Burst Factor Ratings
Engineered using virgin kraft testliners ranging from 120 GSM to 350 GSM, guaranteeing superior Box Compression Test (BCT) scores for multi-tier warehouse palletizing.
JNPT Port Export Readiness
Fully compliant with international maritime container shipping regulations, ISPM-15 wood-free corrugated pallets, and ocean freight shock absorption requirements.
Monsoon-Proof Cobb Control
Surface-treated with food-safe water-repellent emulsions that lower Cobb values below 30 g/m², preventing flute collapse during coastal transit.
Tailored Packaging Solutions for Mumbai’s Primary Industrial Ecosystems
Mumbai’s commercial landscape is exceptionally diverse, requiring specialized corrugated box configurations across different geographic industrial clusters. Our factory engineers customized dielines tailored to the distinct operational realities of Western India:
1. Bhiwandi & Taloja Logistics Corridors (Ecommerce & 3PL Logistics)
As the primary fulfillment centers for major Indian ecommerce platforms and global 3PL operators, warehouses in Bhiwandi require rapid-assembly corrugated boxes. Our tuck-front mailers and auto-bottom shipping cartons eliminate the need for excessive plastic tape, speeding up pack-station throughput while offering structural rigidity capable of surviving multi-drop delivery networks.
2. Thane-Belapur & Tarapur MIDC Chemical & Pharmaceutical Belts
Pharmaceutical exporters operating out of Thane-Belapur MIDC require stringent climate control and contamination-free packaging. We supply cleanroom-compatible, heavy-duty double-wall (BC-flute) and triple-wall corrugated master shippers that protect sensitive liquid vials, bulk active pharmaceutical ingredients (APIs), and medical devices against external shock and thermal fluctuations.
3. BKC, Lower Parel & South Mumbai Luxury D2C & Retail Brands
Direct-to-consumer fashion, jewellery, and gourmet brands based in Mumbai's urban business districts demand an elevated unboxing aesthetic. We manufacture high-definition offset-printed mailer boxes with matte UV lamination, metallic foil stamping, and soft-touch finishes that transform standard corrugated cardboard into a luxury customer touchpoint.
4. Vashi & Navi Mumbai Agricultural & Perishable Food Processing
Serving the massive agricultural trade networks connected to the APMC Market in Vashi, our food-grade corrugated trays and ventilated fresh-produce cartons are manufactured with grease-proof inner barriers. These boxes maintain structural integrity under cold-chain refrigeration and high humidity.
Macro Trends Driving Corrugated Packaging Adoption in Western India
Understanding local market evolutions is critical for procurement managers seeking long-term supply chain efficiency. Key macro dynamics currently reshaping the Mumbai packaging landscape include:
EPR & Maharashtra Plastic Regulations
With the Maharashtra Pollution Control Board (MPCB) strictly enforcing Extended Producer Responsibility (EPR) guidelines, enterprises are rapidly substituting expanded polystyrene (EPS) and bubble wrap with 100% recyclable die-cut corrugated inserts.
Jawaharlal Nehru Port Trust (JNPT) Consolidation
Export shippers operating through JNPT (Nhava Sheva) are upgrading to high-ECT sea-freight master cartons to maximize container volumetric utilization while preventing transit crushing during transoceanic shipping routes.
Q-Commerce & Rapid Fulfillment Packaging
The explosive growth of 10-minute quick-commerce hubs in Mumbai demands compact, tamper-evident kraft paper containers and leak-proof food boxes that resist moisture degradation during bike deliveries.
Engineering Specs: Flute Profiles, Material Physics & Quality Assurance
Our packaging plant operates automated high-speed corrugators capable of producing single-face, single-wall (3-ply), double-wall (5-ply), and triple-wall (7-ply) board combinations. Below is an overview of our core engineering capabilities designed for Mumbai enterprise clients:
| Flute Type | Flute Thickness | Target Application | Key Structural Advantage |
|---|---|---|---|
| E-Flute | 1.1 mm - 1.6 mm | Cosmetics, Gift Mailers, Retail Cartons | Exceptional crush resistance & smooth print surface |
| B-Flute | 2.2 mm - 3.0 mm | Ecommerce Shippers, Food Takeaway Boxes | High puncture resistance & balanced rigidity |
| C-Flute | 3.6 mm - 4.2 mm | Master Shipping Cartons, Industrial Freight | Superior stacking strength & cushioning capacity |
| BC-Flute (Double Wall) | 6.0 mm - 7.0 mm | JNPT Export Cargo, Heavy Machinery Parts | Maximum compression rating for heavy loading |
Every batch of corrugated boxes dispatched from our factory undergoes rigorous Quality Assurance testing in accordance with TAPPI and ISO standards. Our testing protocol includes:
- Bursting Strength Test (BST): Measuring the hydrostatic pressure required to rupture the corrugated board, ensuring box endurance against internal freight pressures.
- Edge Crush Test (ECT): Directly correlating to warehouse pallet stacking limits, guaranteeing your boxes will not buckle under vertical loading in high-bay storage facilities.
- Cobb Water Absorption Test: Verifying that linerboard moisture absorption remains below critical thresholds during humid monsoon transport.
Frequently Asked Questions by Mumbai Buyers & Exporters
What is the minimum order quantity (MOQ) for custom-printed corrugated boxes serving Mumbai?
Our standard Minimum Order Quantity (MOQ) for custom-printed corrugated mailers and folding cartons starts at 250 to 500 units, depending on box dimensions and print complexity. For unprinted standard industrial shipping cartons or large-run enterprise accounts in Bhiwandi or Thane, we accommodate high-volume production schedules with scalable tier pricing.
How do you ensure corrugated boxes do not lose strength during Mumbai’s monsoon season?
We utilize specialized wet-strength additives in our starch adhesives, combined with moisture-resistant sizing on our kraft liners. Additionally, we offer exterior hydrophobic coatings (Cobb rating < 30 g/m²) that prevent water vapor from softening the flute matrix, preserving stacking strength even in high-humidity warehousing.
What are the typical production and delivery lead times to industrial zones like Bhiwandi, Taloja, or Tarapur?
Once structural dielines and 3D digital artwork proofs are approved, standard mass production takes 7 to 10 business days. Expedited direct-to-factory delivery via local freight networks to warehousing hubs across Mumbai, Navi Mumbai, and Thane can be scheduled within 24 to 48 hours post-production completion.
Do you provide ISPM-15 export-compliant corrugated boxes for sea freight via JNPT Port?
Yes. All our export-grade master shippers and heavy-duty corrugated pallets are 100% paper-based and naturally exempt from ISPM-15 phytosanitary wood treatment regulations. They are engineered to endure international ocean transit shock, ocean air humidity, and multi-tier container stacking.
Can you manufacture food-grade takeaway boxes that comply with sanitation standards for Mumbai's F&B sector?
Absolutely. Our food container lines use virgin kraft paperboard certified for direct and indirect food contact. We apply US FDA-compliant aqueous grease-proof liners and soy-based inks, ensuring complete oil resistance without contaminating hot food items.
Can I request a physical structural prototype before approving a full production run?
Yes, we provide CAD-cut physical sample prototypes within 3 to 5 business days. This allows your engineering and packaging teams to perform drop tests, fit tests, and warehouse stacking trials prior to mass manufacturing sign-off.
Ready to Upgrade Your Packaging Supply Chain?
Connect with our structural packaging engineers today. Get a customized dieline, structural CAD sample, and factory-direct wholesale pricing within 24 hours.